What happens between the drawing and the container
Cutting, fit-up, welding, drilling, blasting and coating in one hall — which is why the Bailey panel, the transom and the railing post on the same project can share one welding procedure.
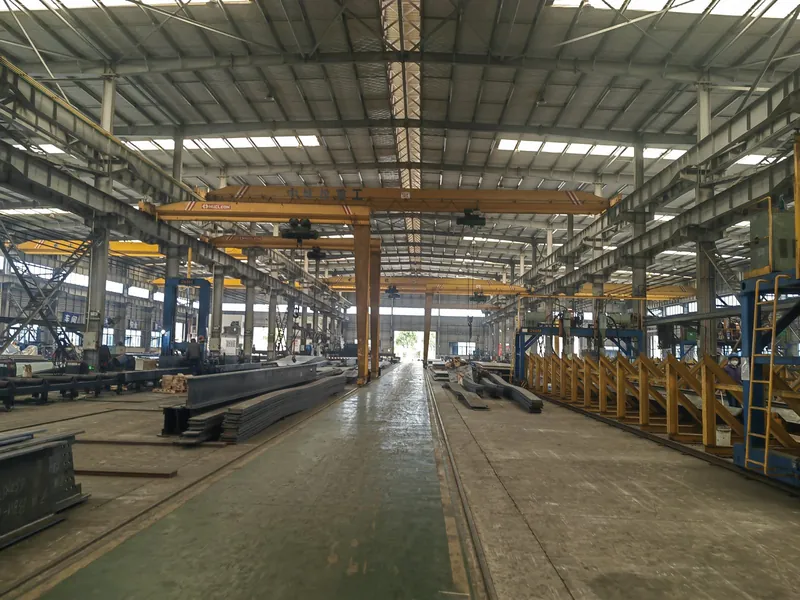
Six steps, each with a check before the next one starts
| Step | What happens | Check before release |
|---|---|---|
| 1. Material | Plate and section cut from coil or stock to the cutting list | Heat number against the mill certificate |
| 2. Cutting | CNC profile cutting, bevelling, edge preparation | Part dimensions and bevel angle |
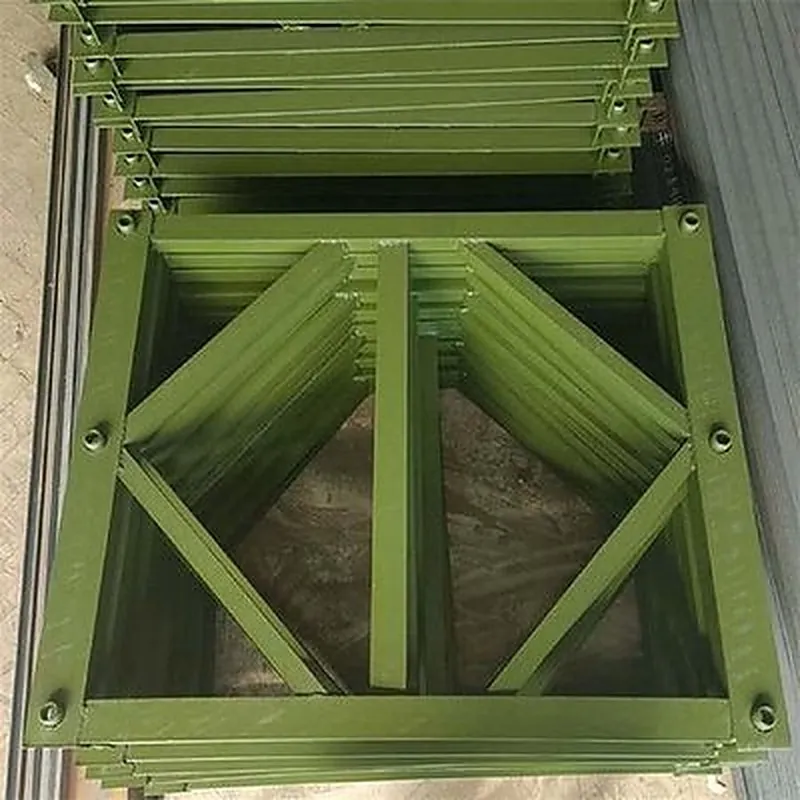
| 3. Fit-up | Jig-based assembly; panels set against a master template | Diagonal, squareness, pin-hole positions |
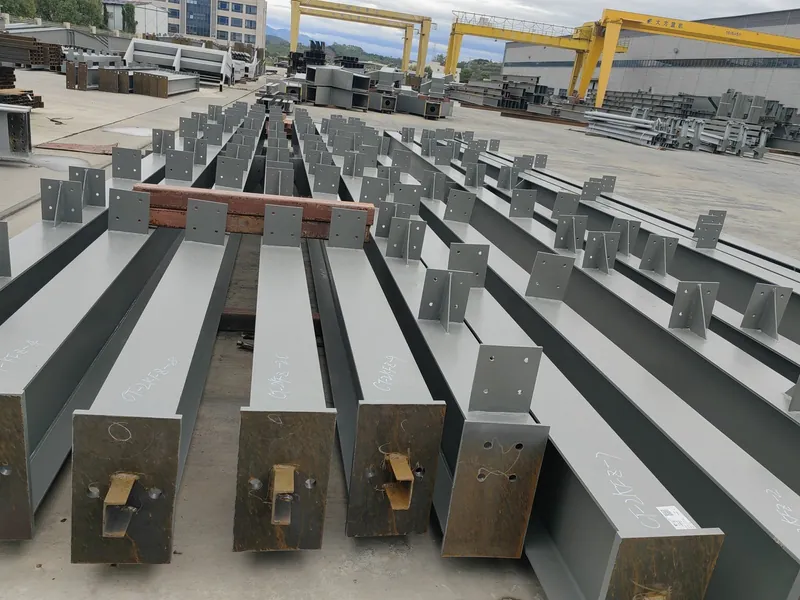
| 4. Welding | SAW for long seams, CO2 for stiffeners and details, to qualified WPS | Weld size, visual inspection, UT or RT where specified |
| 5. Coating | Shot blast to Sa 2.5, primer or hot-dip galvanising, top coat | Surface profile, DFT reading per bundle |
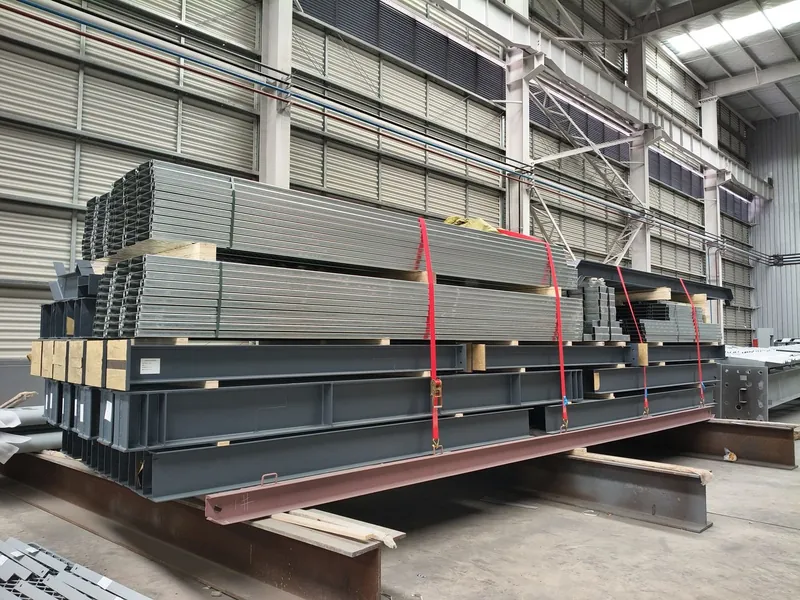
| 6. Packing | Bundling, position marking, packing list, loading plan | Bundle weight, mark against the drawing, photographs |
The machines that decide the tolerance
Most site problems are born in the workshop: a hole that was drilled before welding, a panel that was never trial-assembled, a plate cut on a worn machine. These are the stations that prevent it.
10 t overhead cranes
Long girders and bundled panels can be turned and loaded without hiring a mobile crane, which keeps the dispatch date inside our control.
SAW plus CO2
Submerged-arc for the long straight seams on plate girders and pipe; CO2 for stiffeners, end plates, handrail nodes and repair work.
Drilling after fit-up
Connection holes are drilled on the assembled part, so weld shrinkage does not pull the holes out of line before the panels ever meet on site.
Shot blast to Sa 2.5
Blasting before primer is what makes a coating last. We record surface profile and dry film thickness, bundle by bundle.
Hot-dip galvanising
For coastal and marine work, galvanising at 85 µm minimum. Small and medium items are dipped; long girders are coated with a zinc-rich system.
Export packing
Timber bearers, steel strapping, position marks painted to match the packing list, and a loading plan drawn before the container arrives.
The paperwork that travels with the steel
A buyer cannot see the weld once it is painted. What they can see is the file that arrives with the container — and that file is what a consultant checks when the bridge is handed over.
- Welding procedure specifications and qualification records, held for each process used
- Welder certificates matched to the joints they actually worked on
- Mill certificates for plate and coil, traceable to the heat number marked on the part
- Dimensional inspection record against the approved shop drawing
- Coating thickness record per bundle, with photographs of the loading
Third-party inspection (SGS, BV, CCIC or the client's own surveyor) can be arranged at the workshop before coating and before loading.
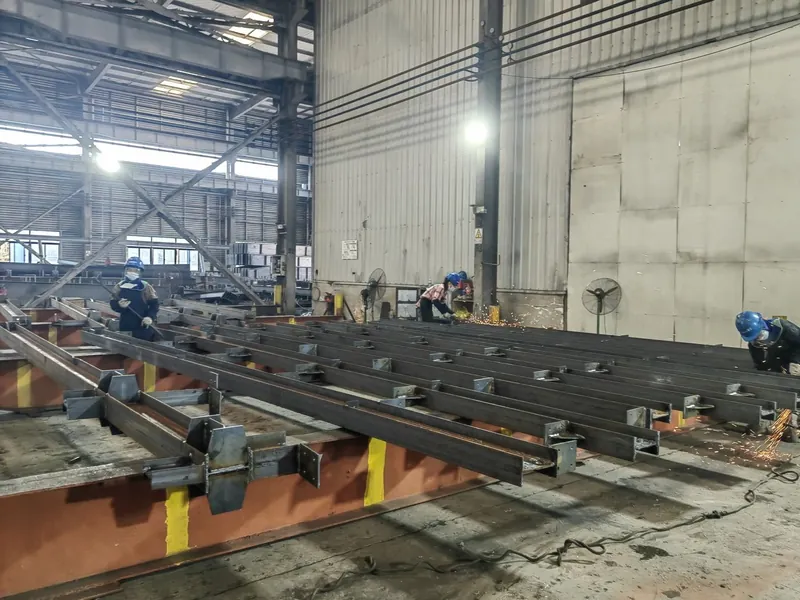
Steel before it becomes a product
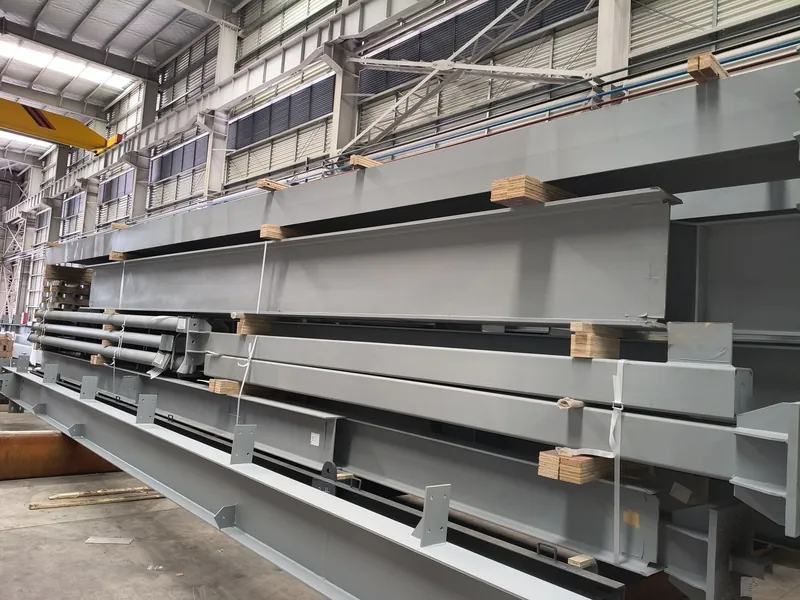
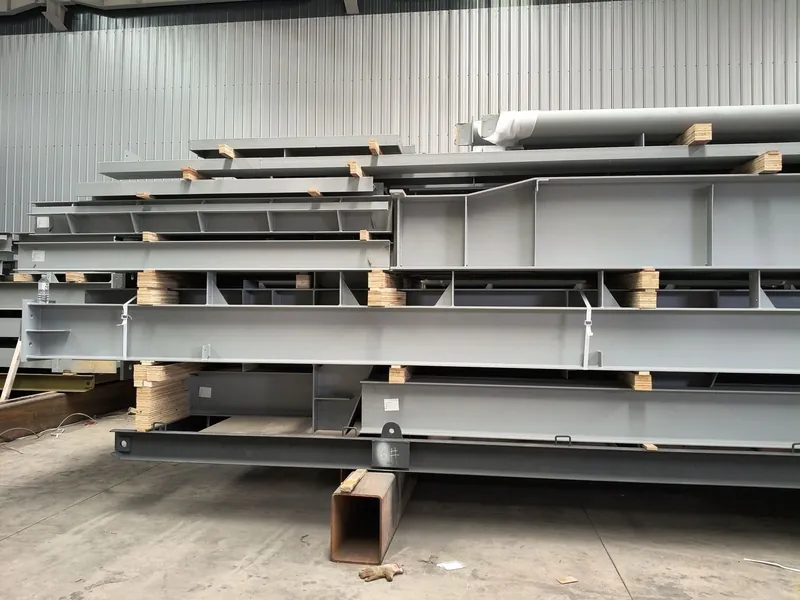
Want to see the workshop before you place the order?
Video walk-through, live call or a third-party audit — all work for us. Ask for the inspection plan at enquiry stage.